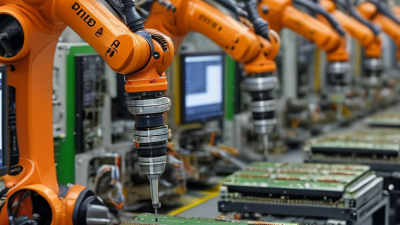
Choosing pcb assembly equipment for global sourcing is not simply a price comparison. It is a production-risk decision involving accuracy, service, software, and long-term support. A fast pick-and-place machine may look attractive, yet weak feeder control can create placement errors, stoppages, and expensive rework.
Michael Ford, a recognized electronics manufacturing strategist, has said, “Data connects the machine to the process, and the process to improvement.” This principle matters when comparing screen printers, SPI systems, placement machines, reflow ovens, AOI, and material-handling tools. Buyers should examine placement accuracy, feeder changeover time, nozzle availability, software compatibility, power requirements, and operator training. Ask for real production data, not only brochure specifications. Request references from factories producing similar board sizes and component mixes.
Global sourcing adds practical complications. A machine may require unusual voltage settings, regional certification, specialized spare parts, or remote support across time zones. A supplier promising delivery in eight weeks may not explain installation delays or unavailable maintenance engineers. That gap deserves attention.
Reliability is built in details.
A strong evaluation also considers total ownership cost. Include shipping, customs, calibration, consumables, software licenses, preventive maintenance, and technician travel. Some assumptions may be wrong. Product volumes can change. Components can become obsolete. Therefore, flexible feeders, open data interfaces, modular upgrades, and responsive support often matter more than headline speed. This guide explains how to compare pcb assembly equipment with clearer evidence, fewer surprises, and a realistic view of global manufacturing conditions.
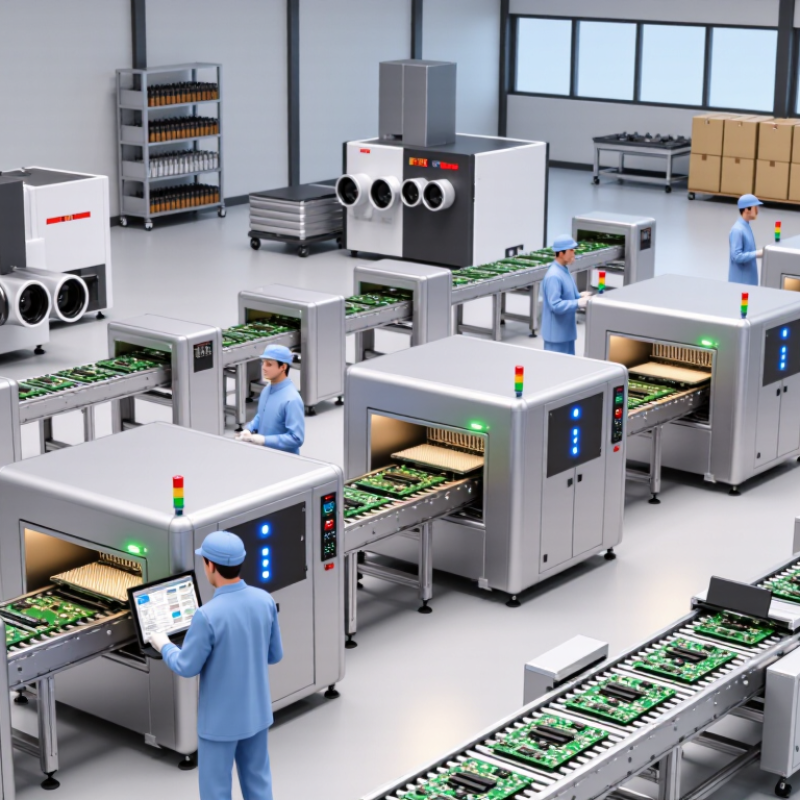
Choosing PCB assembly equipment for global sourcing starts with defining what production must achieve. A machine is useful only when it fits the board, volume, and process. Record board dimensions, component range, placement accuracy, changeover frequency, and expected monthly output. Include soldering methods, inspection needs, and operator skills. Small details matter. A 0.4-millimeter pitch can expose weak process control quickly. I have seen teams purchase for peak capacity, then leave equipment idle during normal weeks. That mistake ties up cash and complicates maintenance.
Sourcing objectives should be measurable before supplier discussions begin. Set targets for cost per board, uptime, first-pass yield, delivery time, training coverage, and spare-parts availability. Separate essential requirements from personal preferences. This prevents attractive quotations from hiding ownership costs. For international projects, verify electrical standards, documentation quality, software support, and local service access. Ask for test reports, calibration records, and a sample production plan. Do not accept vague claims. A video demonstration helps, but it cannot replace a controlled trial using your board files and components.
Use a weighted scorecard and a small pilot order. Assess feeder stability, nozzle wear, inspection repeatability, changeover time, and data traceability. Request written commitments for installation, training, response times, and end-of-life support. The cheapest option may fail the real objective. Yet higher accuracy is not automatically better if your products do not need it. I would also challenge my own forecast; demand estimates often look precise and age badly. Leave room for expansion, but avoid paying today for capacity that remains theoretical.
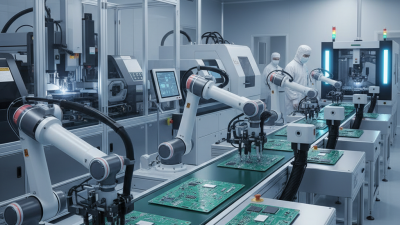
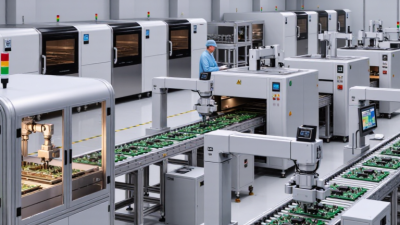
A reliable sourcing decision starts with the product, not the machine catalog. Stencil printers control paste volume and alignment accuracy. Pick-and-place machines determine placement speed, feeder capacity, and component flexibility. Reflow ovens must provide stable temperature zones and repeatable heating. For mixed-technology boards, selective soldering can reduce manual touch-up work. Wave soldering suits many through-hole assemblies, but it needs suitable board layouts.
Inspection equipment adds another layer of control. Solder paste inspection detects printing variation before components are placed. Automated optical inspection checks polarity, missing parts, and visible solder defects. X-ray inspection supports hidden joints, such as bottom-terminated packages. Ask suppliers about data traceability, changeover time, calibration records, and operator training. These details often affect delivery performance more than advertised speed.
Tips: Match equipment capability with real production volume and product diversity. I have seen teams overbuy high-speed systems, then struggle with frequent changeovers. That is an expensive lesson. Check local voltage requirements, spare-part access, software support, and safety documentation before purchasing. Request sample runs using your smallest components, largest connectors, and most difficult board. A short trial may reveal feeder errors or thermal limits that brochures never mention. Leave room for improvement, but do not pay for capacity you cannot verify.
Choosing PCB assembly equipment requires more than comparing purchase prices. The supplier must understand your board designs, production volume, and component mix. Ask whether the equipment handles your smallest packages, board thickness, and maximum panel size. Confirm software compatibility with your existing design and production files. A smooth data exchange can prevent hours of manual correction.
Quality evidence matters. Request calibration records, inspection procedures, and sample production reports. Reliable suppliers should explain how they control placement accuracy, solder quality, and equipment maintenance. During a factory visit, inspect cable labeling, feeder storage, and machine cleanliness. Small details often reveal daily discipline.
I once focused heavily on machine specifications and overlooked spare-part availability. That decision created avoidable delays.
Technical support becomes critical across time zones. Check response times, remote diagnostic methods, training options, and local service coverage. Ask for a clear escalation process when production stops. A useful supplier can guide operators through alarms using precise instructions, not vague promises. Confirm the availability of replacement parts and preventive-maintenance schedules before signing.
Support quality is difficult to measure from a sales presentation. Test it with practical questions. Their answers may expose gaps. Also, request references from manufacturers with similar products and production conditions.
A supplier can appear highly capable, yet lack experience with your assembly complexity. Be willing to revise your evaluation criteria when testing reveals weaknesses.
Choosing PCB assembly equipment for global sourcing requires more than comparing purchase prices. Calculate the landed cost: equipment, freight, insurance, duties, local taxes, installation, training, calibration, energy, spare parts, and downtime. The World Bank’s 2023 Logistics Performance Index evaluated 139 economies, showing major differences in customs efficiency and shipment reliability. A cheaper machine can become expensive after delays and weak local service.
Compliance must be checked before signing a purchase order. Request conformity documents for machinery safety, electromagnetic compatibility, electrical safety, and substance restrictions. Confirm whether the destination requires local testing or registration. IPC standards can support process qualification, but they do not replace national legal requirements. Keep serial numbers, certificates, software versions, and maintenance records together. Small omissions create large delays.
Logistics needs equal attention. UNCTAD’s Review of Maritime Transport reports that over 80% of global merchandise trade moves by sea, making packaging and transit planning essential. Specify moisture barriers, shock indicators, lifting points, and a delivery inspection procedure. Verify HS classification and Incoterms with a qualified customs adviser. I would also budget for exchange-rate movement and one urgent spare shipment. That estimate may still be wrong. Real factories expose hidden costs, especially during installation. A pilot line, acceptance test, and written service response time provide stronger evidence than a polished quotation.
A reliable equipment plan begins with the product, not the machine catalogue. Define board dimensions, component ranges, placement density, throughput, changeover frequency, and expected production volume. I have seen teams overbuy capacity, then struggle with unnecessary maintenance and unused functions. Create a process map from solder paste printing through inspection and rework. Record each critical tolerance.
Request documented performance data from several qualified suppliers. Compare placement accuracy, feeder stability, inspection coverage, software compatibility, energy use, and operator training. Ask for sample-board trials using your actual materials and smallest components. A factory acceptance test should verify speed, repeatability, alarms, traceability, and recipe control. Do not accept attractive laboratory results without production evidence. That mistake is common.
Tips: Build a scoring sheet with weighted requirements. Check calibration records and service response times. Confirm spare-part availability in each sourcing region. Test data exports before signing. Include operators during trials; their feedback may expose awkward loading, unclear alarms, or unsafe movement. Validate a complete pilot run, not only individual machines. Measure defects, downtime, changeovers, and operator intervention. Document every result with photos and serial references. Keep one assumption visible for review, because early estimates are often wrong.